In many factories, the production plan lives in one planner's Excel file and head. It works — until orders change, a machine breaks down, material is late, or the planner is on leave. Then the factory runs on phone calls. Production planning and scheduling software makes the plan visible, keeps it up to date with what actually happens, and helps the planner decide quickly when things change.
This guide explains how custom production planning software is designed and developed, what it should include, and how to introduce it without disrupting production. For background, see production planning software: from Excel to scheduling.
Levels of planning
- Sales and operations planning — monthly or quarterly: demand versus capacity, hiring, overtime, stock building.
- Master production schedule — weekly: what to produce by product and period.
- Material requirements planning — what materials to buy or make, and when. See MRP explained.
- Detailed scheduling — daily or by shift: which job on which machine in which sequence. See finite capacity scheduling.
- Execution and feedback — the shop floor reports progress, and the plan adjusts.
Most small and mid-sized factories need the last three most urgently.
Core modules
Order intake and demand
Sales orders, customer schedules, blanket order call-offs and forecasts in one place, with due dates and priorities. For make-to-stock items, replenishment needs based on stock and forecasts. See make-to-order versus make-to-stock.
Product data
BOMs and routings with machines or work centres, setup and cycle times, alternate machines, batch sizes and lead times for outside operations.
Capacity
Machines and work centres with shifts, holidays, planned maintenance and efficiency. Load versus capacity by week or day shows overloads before they become late orders.
Material planning
Requirements exploded from orders through BOMs, netted against stock and open purchase orders, with suggested purchase and production orders. Shortages are flagged against the jobs they affect.
The planning board
A visual board — machines down the side, time across — where jobs are placed, sequenced and moved by drag and drop. The system checks material availability, tooling, predecessors and capacity, and warns about conflicts and late jobs.
Scheduling rules
Rules that reflect your factory: group jobs by colour, material or tooling to reduce changeovers; respect operator skills; keep a machine free for urgent orders; follow customer priority. The system can propose a sequence; the planner adjusts.
Release and dispatch lists
Each machine or line gets its job list for the shift, on a tablet or printout, in the planned sequence.
Feedback and replanning
Progress from MES booking or machine monitoring updates the board. Breakdowns, rejections and late material trigger replanning. See closing the loop between planning and MES.
Delivery promising
Sales can see realistic completion dates and test "what if we accept this order?" against current load.
Designing around your constraints
Discovery for a planning system should capture what actually limits your output:
- Bottleneck machines and their changeover times.
- Tooling — moulds, dies, fixtures — that can be on only one machine at a time.
- Operators with specific skills or certifications.
- Outside operations such as heat treatment, plating or painting, with vendor lead times.
- Batch processes with minimum and maximum sizes, or curing and drying times.
- Customer priorities and penalties for lateness.
Only the constraints that really matter should be modelled — every extra rule adds complexity.
Integrations
- ERP or Tally — sales orders in, purchase suggestions out.
- Inventory — stock and open purchase orders for material checks.
- MES / shop-floor booking — progress and actual times.
- Maintenance — planned maintenance windows and breakdowns.
- Customer portals or EDI — schedules from large customers.
Rollout
- Clean routings, standard times and machine lists.
- Start with order intake, capacity view and the planning board, replacing the Excel plan.
- Add shop-floor feedback so the plan reflects reality.
- Add material planning when BOMs and stock are reliable.
- Introduce scheduling rules and automated suggestions step by step.
What drives development cost
- Planning depth — a visual board is simpler than automated optimisation.
- Number and complexity of constraints.
- MRP scope — single-level versus multi-level BOMs, alternates and lot sizing.
- Integrations with ERP, inventory, MES and customer systems.
- Volume — number of machines, jobs and operations.
- Reporting and delivery promising.
Signs it is working
- Everyone sees the same plan, updated in real time.
- On-time delivery improves; late orders are known in advance.
- Changeovers fall because jobs are sequenced deliberately.
- Material shortages are flagged days ahead, not on the day.
- The plan survives the planner's day off.
A worked example: a plastic injection moulding company
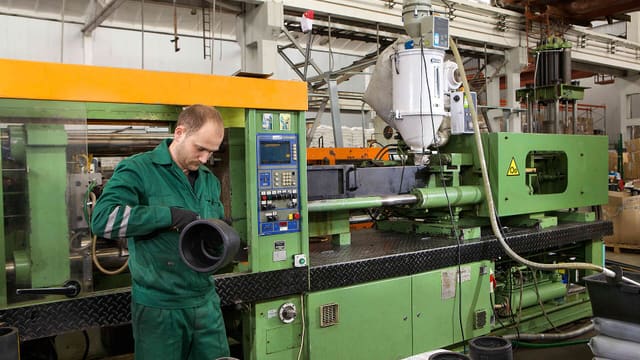
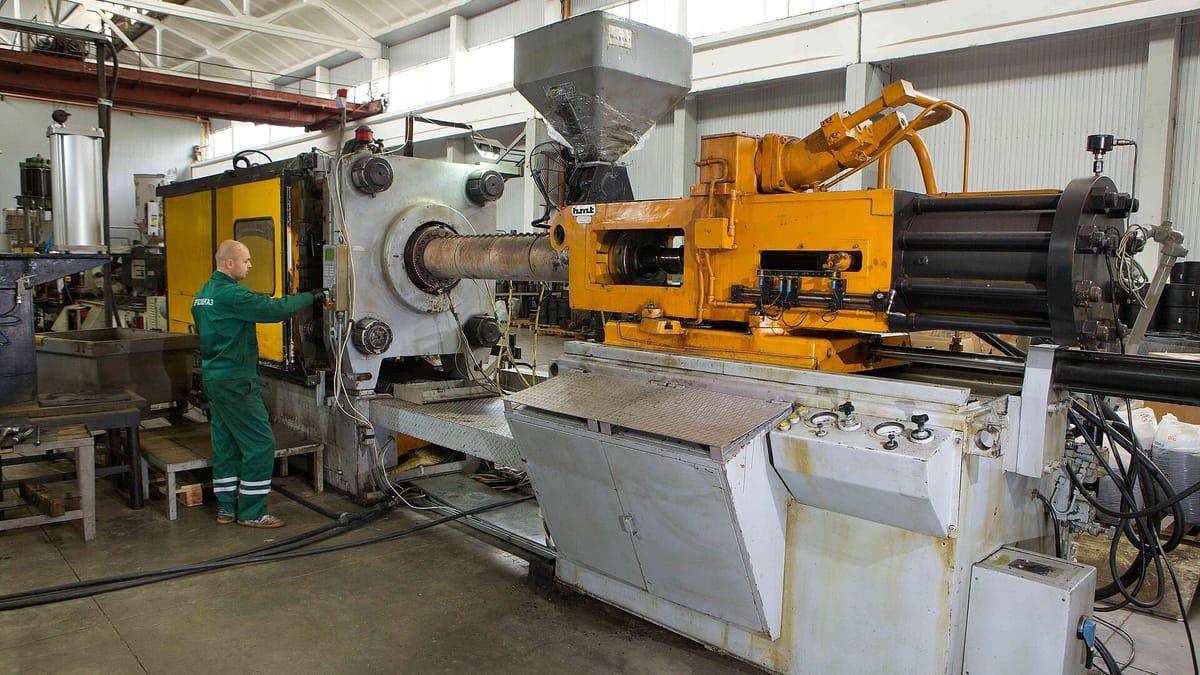
A moulder with 30 machines and 200 active moulds planned on a whiteboard and an Excel sheet. Problems included frequent colour changes that wasted material, moulds scheduled on machines that could not take them, and late discovery that a mould was under maintenance.
The planning system holds which machines each mould can run on, colour and material for each job, and mould availability from the maintenance system. The planner drags jobs onto machines on a board; the system warns if the mould is unavailable or the machine is unsuitable, and suggests a sequence from light to dark colours. Actual shots from the shop floor update progress, so delays show immediately. Changeover material waste and late orders both fall. See MES for plastics and injection moulding.
Scheduling approaches
| Approach | How it works | When it fits |
|---|---|---|
| Manual board with checks | Planner places jobs; software checks conflicts | Most SMEs; high planner knowledge |
| Rule-based sequencing | Software orders jobs by due date, family, priority | Repetitive changeover patterns |
| Finite capacity scheduling | Software loads jobs respecting capacity and constraints | Many machines and operations |
| Optimisation | Software searches for best sequence against objectives | Complex, high-volume environments |
Start with the simplest approach that solves your problem; planners trust tools they understand.
Common mistakes
- Inaccurate standard times — the plan is only as good as setup and cycle times; correct them with shop-floor data.
- No feedback loop — without actual progress, the plan diverges from reality within a day.
- Over-modelling — encoding every rule makes the system rigid and slow to change.
- Planning without material — schedules that ignore material availability create false expectations.
- Bypassing the plan — urgent changes made verbally on the floor and not in the system.
Working with Corposol
Corposol is a manufacturing software development company founded in 2018 in Bengaluru, India, with a US company, Corposol LLC, in Montana. We build production planning and scheduling software as cloud web applications with Android and iOS apps where they help, connect them to the systems you already use where those systems allow it, deliver in phases, and transfer all custom code to you on final payment. If you are planning a project, we are happy to walk through your current process and suggest a sensible first phase.
Frequently asked questions
Why do factories build their own planning software?
Planning rules are where factories differ most: changeovers, tooling constraints, operator skills, job work lead times, customer priorities and batch sizes. Generic planning tools often cannot reflect them, so planners fall back on Excel. Custom software can encode the rules that matter.
Does the software create the plan automatically?
It can propose a schedule based on rules and constraints, but most factories keep the planner in control. The best systems suggest, check feasibility and highlight conflicts, while the planner decides.
How does planning software get actual progress?
From production booking in an MES or shop-floor app, or from machine monitoring. Without real progress, the plan quickly becomes fiction.
Can we start without MRP?
Yes. Many factories start with order intake, a capacity view and a planning board, then add material planning once BOMs and stock records are reliable.